Clear PP Sheet for Vacuum Forming & Thermoforming
HSQY clear polypropylene sheet is an extruded PP material for vacuum forming and thermoforming, available in 0.08-3mm thickness with customized widths for trays, packaging inserts, clamshells and other formed plastic products.
Transparent polypropylene combines low material density, low moisture absorption, useful chemical resistance and flexible processing characteristics. High-clarity PP grades can also provide improved product visibility for thermoformed packaging and display applications.
For vacuum-forming buyers, material selection should consider starting thickness, machine width, cavity depth, mold geometry, required wall distribution, clarity after forming and the final application rather than choosing sheet by price or nominal gauge alone.
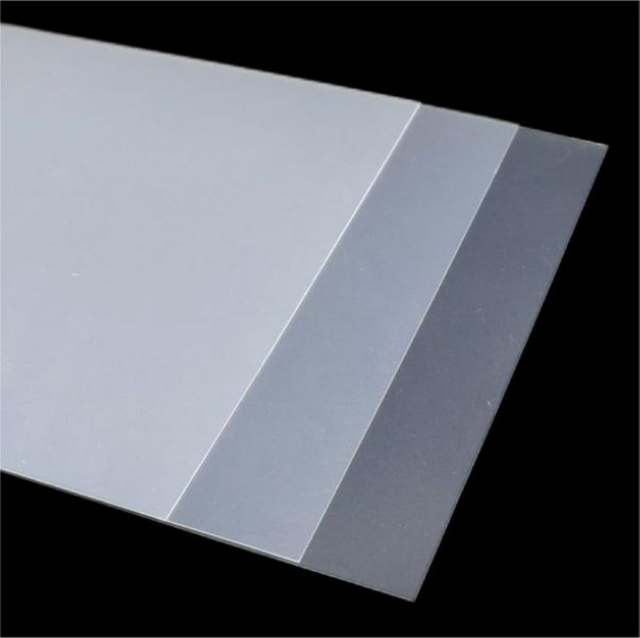
Clear Polypropylene Sheet Images
")
Clear PP Sheet for Vacuum Forming
")
Transparent PP Thermoforming Sheet

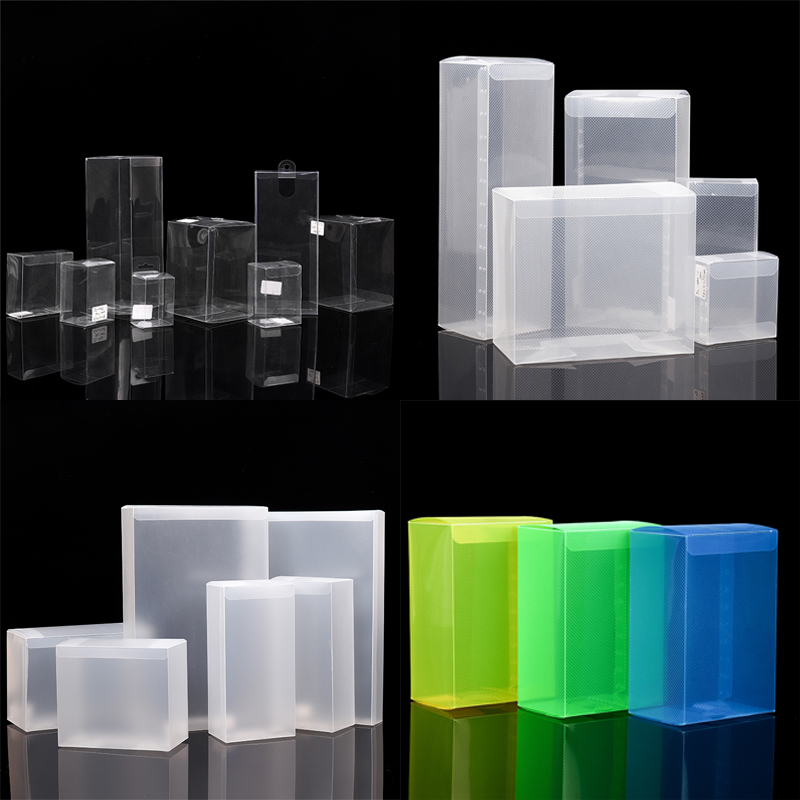
Polypropylene Sheet for Forming & Fabrication
Clear PP Sheet Specifications
| Property |
Specification |
| Product |
Clear Polypropylene Sheet for Vacuum Forming |
| Material |
Polypropylene Plastic (PP) |
| Color |
Clear |
| Thickness |
0.08mm-3mm |
| Width |
Customized |
| Type |
Extruded |
| Main Processing |
Vacuum Forming, Thermoforming, Cutting and Fabrication according to project requirements |
| Main Application Direction |
Thermoformed trays, packaging inserts, clamshells, covers, protective packaging and formed components |
| Other Listed Applications |
Food, medical, industrial, electronics and advertising applications subject to the appropriate PP grade and documentation |
Specification Note: The current HSQY page does not publish maximum roll width, roll diameter, core diameter, roll weight, thickness tolerance or a recommended thermoforming temperature window. Buyers requiring these parameters should provide their equipment specification for production confirmation.
What Is Clear PP Sheet for Vacuum Forming?
Clear PP sheet for vacuum forming is an extruded polypropylene sheet that is heated until it becomes formable and then shaped against a mold using vacuum pressure.
After the formed part cools, it retains the mold geometry and can be trimmed into trays, inserts, lids, clamshell components or other three-dimensional parts.
PP is a semi-crystalline polymer, so forming behavior and transparency are influenced by resin formulation, heating profile, crystallization, sheet thickness, mold design and cooling conditions. Stable processing therefore requires a thermoforming-grade specification matched to the actual production line.
Vacuum Forming vs. Thermoforming
| Process |
How It Works |
Buyer Consideration |
| Thermoforming |
General process of heating thermoplastic sheet and shaping it over or into a mold |
Covers vacuum forming, pressure forming and related forming methods |
| Vacuum Forming |
Uses vacuum to pull heated sheet against the mold surface |
Common for trays, inserts, packaging and relatively straightforward formed geometries |
| Pressure Forming |
Uses additional air pressure to force the sheet against the mold |
Can be considered where more defined surface detail is required |
Why Use Polypropylene for Vacuum Forming?
| PP Property |
Relevance to Formed Products |
| Low Density |
Helps reduce finished-part weight compared with denser plastics |
| Low Moisture Absorption |
Useful for packaging and products used in humid environments |
| Chemical Resistance |
PP offers useful resistance to many chemicals, although compatibility must be checked for the exact substance and conditions |
| Thermoformability |
Suitable grades can be shaped into trays, inserts and other three-dimensional parts |
| Toughness |
Provides useful handling and impact performance in suitable formed products |
| Clear Grade Availability |
High-clarity PP formulations can provide improved product visibility where transparency is important |
Thermoforming Performance: What Buyers Should Evaluate
Polypropylene generally requires closer control of thermoforming conditions than some common amorphous packaging plastics. The forming trial should therefore evaluate the complete process rather than only whether the starting sheet becomes soft enough to form.
| Forming Factor |
Why It Matters |
| Heating Uniformity |
Uneven heating can cause inconsistent forming and wall distribution |
| Sheet Sag |
Must be controlled so the sheet enters the forming stage consistently |
| Draw Depth |
Deeper cavities can increase wall thinning and require a different starting thickness |
| Corner Geometry |
Tight corners and small radii can create localized thinning |
| Cooling |
Cooling conditions influence dimensional stability, crystallization and appearance |
| Trimming |
Finished parts should be evaluated for clean trimming and dimensional repeatability |
| Formed Clarity |
Optical appearance can change after heating and stretching |
0.08mm to 3mm Clear PP Sheet
The current HSQY product specification covers thicknesses from approximately 0.08mm to 3mm. The appropriate starting gauge depends on finished-part size, forming depth, rigidity requirement and minimum acceptable wall thickness after forming.
| Thickness Direction |
General Processing Direction |
| 0.08-0.2mm |
Thin converting and lightweight applications subject to the forming capability of the selected grade |
| 0.25-0.5mm |
Lightweight formed packaging, inserts and relatively shallow parts |
| 0.6-1mm |
Trays, clamshell components and formed parts requiring greater rigidity |
| Above 1mm |
Thicker formed and fabricated parts where the selected production specification supports the required gauge |
These are general application directions, not fixed thermoforming limits. Final starting thickness should be evaluated against mold geometry and finished-part requirements.
Clear PP for Shallow & Deep Forming
Shallow trays and simple packaging geometries generally place less demand on material distribution than deep cavities or parts with narrow corners.
For deeper forming, buyers should provide mold dimensions, cavity depth and required minimum wall thickness. Plug assist, pressure forming or another forming method may also be evaluated depending on the package geometry and production equipment.
HSQY's current public page does not provide a maximum recommended draw ratio, so this value should be established through technical confirmation or a forming trial rather than assumed.
Clarity After Vacuum Forming
The original page describes the material as having near-glass transparency. For technical purchasing, it is more accurate to describe the product as clear or high-clarity PP because polypropylene is a semi-crystalline material and optical performance depends on formulation and processing.
Heating and stretching during thermoforming can change haze, gloss and transparency. Buyers producing transparent retail packaging should therefore approve the material after forming rather than evaluate only the flat starting sheet.
If optical appearance is critical, provide the required haze, light transmission or gloss specification and request corresponding data or production samples for the selected thickness.
Clear PP vs. PET for Thermoforming
| Selection Factor |
Clear PP |
Clear PET / APET |
| Transparency |
High-clarity PP grades can provide good transparency, but appearance depends strongly on crystallization and processing |
Widely selected for high-clarity conventional thermoformed packaging |
| Density |
Lower-density polymer |
Higher density than PP |
| Thermoforming Process |
Requires controlled heating and suitable thermoforming-grade formulation |
Commonly processed for clear thermoformed packaging |
| Heat Direction |
Suitable PP grades can be selected where greater heat performance is required |
Standard APET is typically used for conventional ambient and chilled packaging applications |
| Moisture Absorption |
Very low moisture absorption |
Different moisture behavior and barrier profile from PP |
| Best Material |
Depends on required transparency, forming process, heat exposure, stiffness, package geometry, sealing and regulatory requirements. |
Packaging & Tray Applications
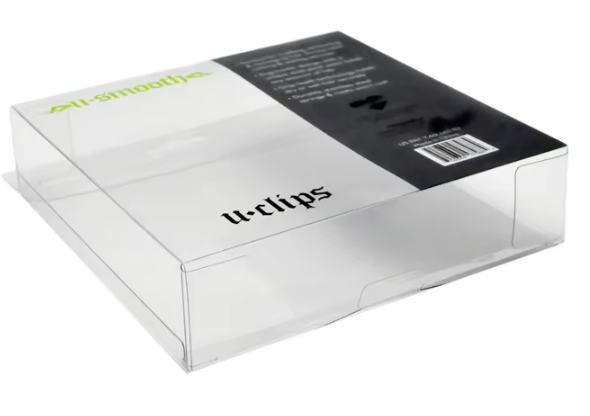
Clear thermoforming PP can be evaluated for trays, inserts, clamshell components, protective packaging, lids and other formed packaging products.
For packaging projects, provide the finished part dimensions, mold design, forming depth, expected temperature exposure and sealing requirements. Food-contact packaging also requires the appropriate food-contact PP grade and supporting documentation.
Food Packaging Applications
The original HSQY page lists food applications and references FDA food-contact compliance. This should be confirmed for the exact polypropylene resin grade and finished sheet supplied to the buyer.
For direct food contact, provide the food type, contact temperature, heating conditions, storage conditions and destination-market standard. If FDA, EU food-contact or another document is required, confirm the applicable product-level documentation before commercial approval.
Medical & Laboratory Thermoforming
The original application list includes medical and laboratory products. These uses require a suitable PP grade when sterilization, cleanliness, biocompatibility, extractables or other regulated requirements apply.
A standard clear PP sheet should not automatically be described as medical-grade or sterile. Medical projects should provide the intended product, sterilization method and required documentation before material selection.
Electronics & ESD Thermoforming Applications
Polypropylene can also be thermoformed into component trays and protective packaging for suitable electronics applications.
Standard clear PP should not automatically be treated as antistatic. Electronics packaging that requires electrostatic-discharge protection should specify an antistatic, dissipative or conductive grade together with the required surface-resistance range.
Printing & Surface Treatment
Polypropylene has relatively low surface energy. Printing, coating, lamination or adhesive bonding can therefore require corona treatment, flame treatment, primer or another appropriate surface-treatment method.
If the formed part will be printed or labeled, provide the ink, adhesive or converting process together with any required treated-side or surface-energy specification.
Chemical Resistance
Polypropylene offers useful resistance to many acids, alkalis, oils and other chemicals, which supports its use in packaging and selected industrial applications.
Chemical compatibility should be confirmed according to the specific chemical, concentration, exposure time and temperature. The original broad solvent-resistance claim should not be interpreted as universal resistance to all solvents.
Moisture Resistance
Polypropylene has very low moisture absorption and is widely used where resistance to humid conditions is valuable.
The original page uses the phrase “zero water absorption.” For technical purchasing, “very low moisture absorption” is more appropriate unless a standardized test result is available for the exact grade.
UV-Stabilized PP Options
The original product information states that UV-stabilized options are available. UV resistance should be treated as an application-specific grade requirement rather than an inherent property of every clear PP sheet.
For outdoor formed products, specify the expected sunlight exposure, required service environment and any accelerated-weathering requirements before selecting the grade.
Recyclability Considerations
Polypropylene is a thermoplastic that can be mechanically recycled where suitable collection, sorting and processing infrastructure exists.
The original page describes the material as 100% recyclable. In practice, recyclability of the finished product depends on inks, labels, adhesives, coatings, other materials, contamination and the local recycling system.
Other Listed Clear PP Applications
| Application Area |
Selection Note |
| Packaging |
Trays, clamshells, inserts and protective packaging are suitable forming directions |
| Medical & Laboratory |
Requires a suitable grade and relevant regulatory or sterilization documentation |
| Printing & Signage |
Surface treatment and ink adhesion should be confirmed |
| Industrial |
Mechanical loads, chemical exposure and finished-part geometry should be evaluated separately |
| Retail & Advertising |
Suitable for selected product displays and formed presentation components |
| Architecture |
Partitions and other building applications require the appropriate thickness and structural design |
| Electronics |
Standard PP should not be described as antistatic without a defined ESD grade |
Critical PP Sheet Parameters for Thermoformers
| Parameter |
Why It Matters |
| Thickness |
Determines starting gauge and influences final wall thickness |
| Thickness Tolerance |
Stable gauge improves repeatability during forming |
| Width |
Must match the thermoforming line and mold layout |
| Roll Diameter |
Must fit the unwind system and production-line limitations |
| Core Diameter |
Must match the buyer's shaft or chuck where rollstock is used |
| Winding Quality |
Poor winding can cause wrinkles, edge damage or line-feeding problems |
| Clarity / Haze |
Important for transparent packaging and visible retail products |
| Surface Treatment |
Relevant for printing, coating, adhesive bonding and labeling |
| Functional Grade |
Food-contact, medical, antistatic or UV requirements must be defined before production |
What Information Should You Provide for a Quote?
| Requirement |
Information to Provide |
| End Product |
Tray, insert, clamshell, cover, industrial part or other formed product |
| Thickness |
Required starting thickness within the listed 0.08-3mm range |
| Width |
Required sheet or roll width |
| Supply Form |
Roll or cut sheet according to production requirements |
| Roll Specification |
Outside diameter, core diameter and maximum roll weight where applicable |
| Forming Process |
Vacuum forming, pressure forming or other thermoforming method |
| Mold Geometry |
Cavity length, width, depth, corner radius and number of cavities |
| Finished Wall Requirement |
Required minimum wall thickness or rigidity after forming |
| Optical Requirement |
Required clarity, haze or gloss after forming |
| Surface Treatment |
Printing, corona, coating or adhesive requirements where applicable |
| Functional Grade |
Food-contact, medical, antistatic, conductive or UV-stabilized requirements |
| Documentation |
Required food-contact, SGS or other applicable compliance documents |
| Quantity |
Trial requirement and expected production volume |
| Destination |
Country and destination port |
Frequently Asked Questions About Clear PP Vacuum Forming Sheet
Can polypropylene sheet be vacuum formed?
Yes. Suitable PP grades can be heated and vacuum formed into trays, inserts, clamshell components and other three-dimensional parts. Forming quality depends on resin grade, heating conditions, mold geometry and starting thickness.
What is the difference between vacuum forming and thermoforming?
Thermoforming is the broader process of heating and shaping thermoplastic sheet. Vacuum forming is a type of thermoforming that uses vacuum pressure to pull the heated sheet against a mold.
What PP sheet thicknesses does HSQY list?
The current HSQY product specification lists 0.08mm to 3mm.
Can the width be customized?
Yes. The current product information lists customized width. Provide your thermoforming machine width and required finished web width for confirmation.
Is the material supplied in rolls or sheets?
The current source does not publish a fixed supply format for every configuration. Specify whether your production line requires rollstock or cut sheets when requesting a quotation.
What roll core and roll diameter are available?
The current HSQY page does not publish these values. Provide the required core diameter, maximum roll outside diameter and maximum roll weight for production confirmation.
Is clear PP as transparent as PET?
Not necessarily. High-clarity PP can provide good transparency, but optical performance depends on resin formulation, crystallization and processing. PET is commonly selected when very high conventional packaging clarity is the priority.
Does transparency change after thermoforming?
It can. Heating, stretching, cooling and crystallization can influence haze and gloss. Evaluate a formed sample when the finished part requires a specific optical appearance.
Can clear PP be used for deep-draw forming?
Suitable PP grades can be evaluated for deeper forming, but cavity depth, wall thinning, corner geometry and machine configuration must be considered. Provide the mold dimensions before selecting the starting thickness.
What forming temperature should I use?
The current HSQY public specification does not provide a validated forming-temperature range. The correct heating profile depends on resin grade, thickness, equipment and mold geometry and should be established using the technical data for the supplied material.
Can this PP sheet be used for food trays?
Suitable food-contact PP grades can be thermoformed into food trays and containers. Confirm the exact grade and applicable food-contact documentation required for the destination market.
Is this PP sheet FDA compliant?
The original page references FDA food-contact compliance. Buyers should request the applicable documentation for the exact resin grade and finished sheet being supplied rather than applying that statement to every configuration.
Can clear PP be used for medical thermoforming?
Medical applications require an appropriate PP grade and project-specific documentation. Provide sterilization, cleanliness and regulatory requirements before material selection.
Is standard clear PP antistatic?
No defined antistatic performance should be assumed for standard clear PP. Electronics trays requiring ESD protection should specify an antistatic, dissipative or conductive grade and target resistance range.
Does PP absorb water?
Polypropylene has very low moisture absorption, making it useful for many packaging and humid-environment applications.
Is PP chemically resistant?
PP provides useful resistance to many acids, alkalis and chemicals, but compatibility should be checked for the specific substance, concentration, temperature and exposure time.
Are UV-stabilized grades available?
The original page lists UV-stabilized options. Outdoor service requirements should be specified separately because UV resistance is not automatically a standard property of every clear PP grade.
Is clear PP recyclable?
PP can be mechanically recycled where suitable collection and recycling infrastructure exists. Actual recyclability of the finished product depends on additional materials and local recycling systems.
What should I provide for a quotation?
Provide the end product, starting thickness, width, roll or sheet requirement, core and roll diameter if applicable, forming method, mold dimensions, cavity depth, clarity requirement, functional grade, quantity and destination.
Packing
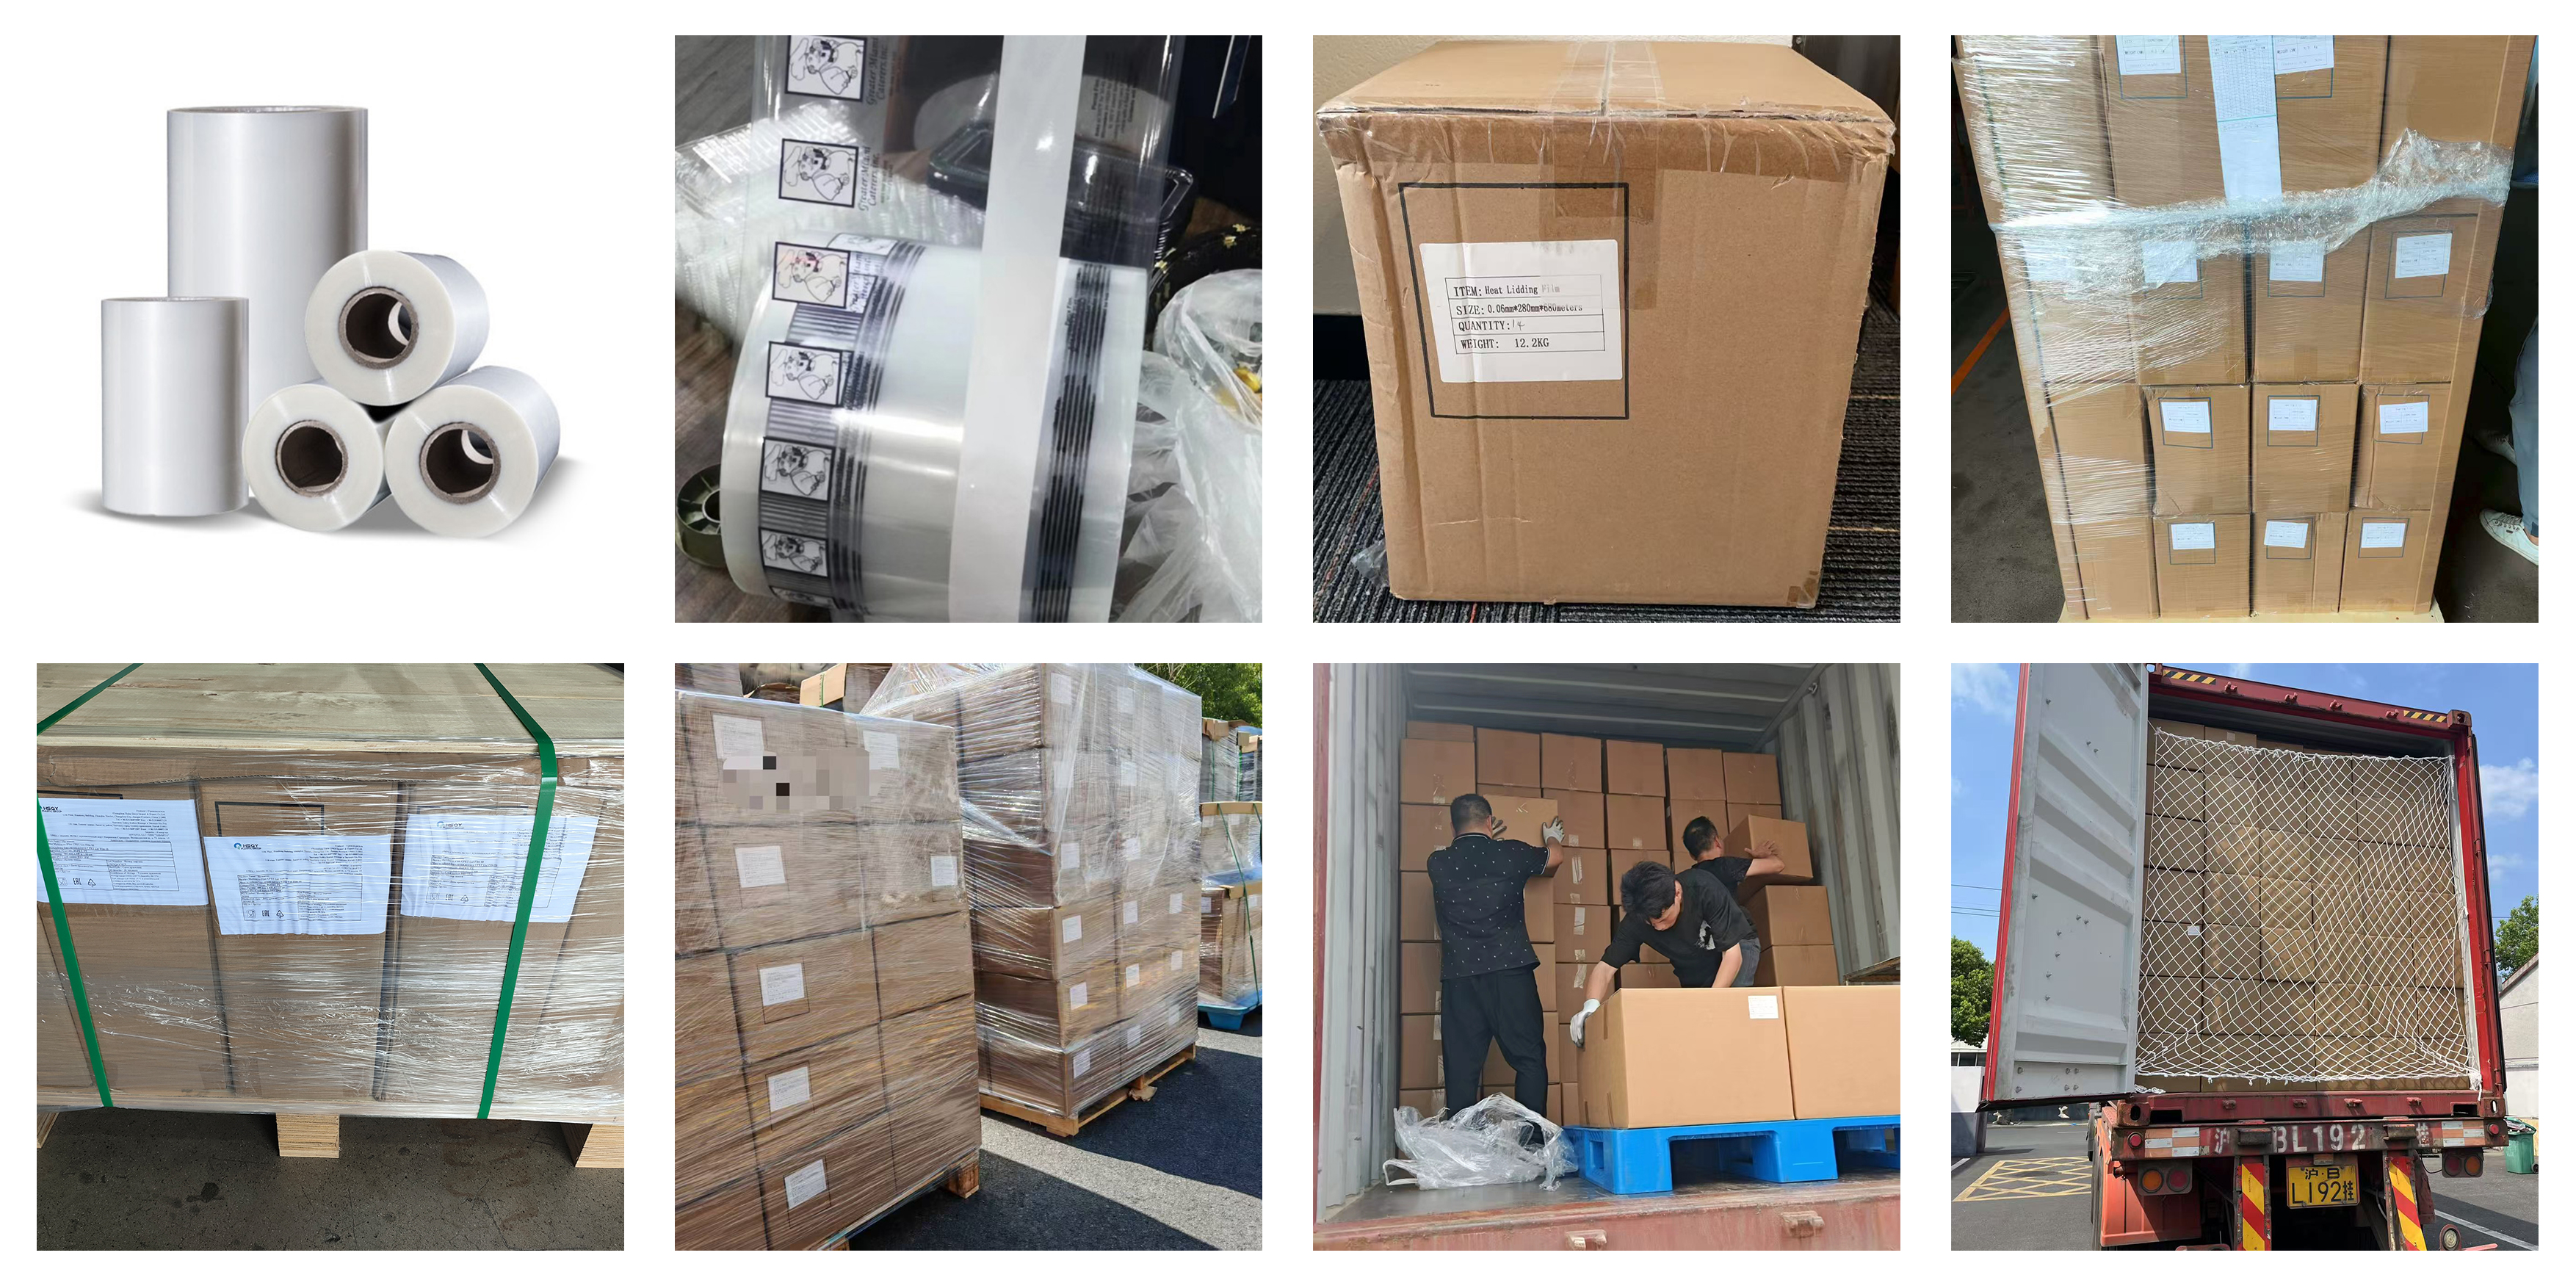
Packing should protect clear PP surfaces and sheet edges from contamination, scratching and handling damage during storage and transportation. Confirm the required roll or sheet packing format according to the final specification.

Clear Polypropylene Sheet Packing
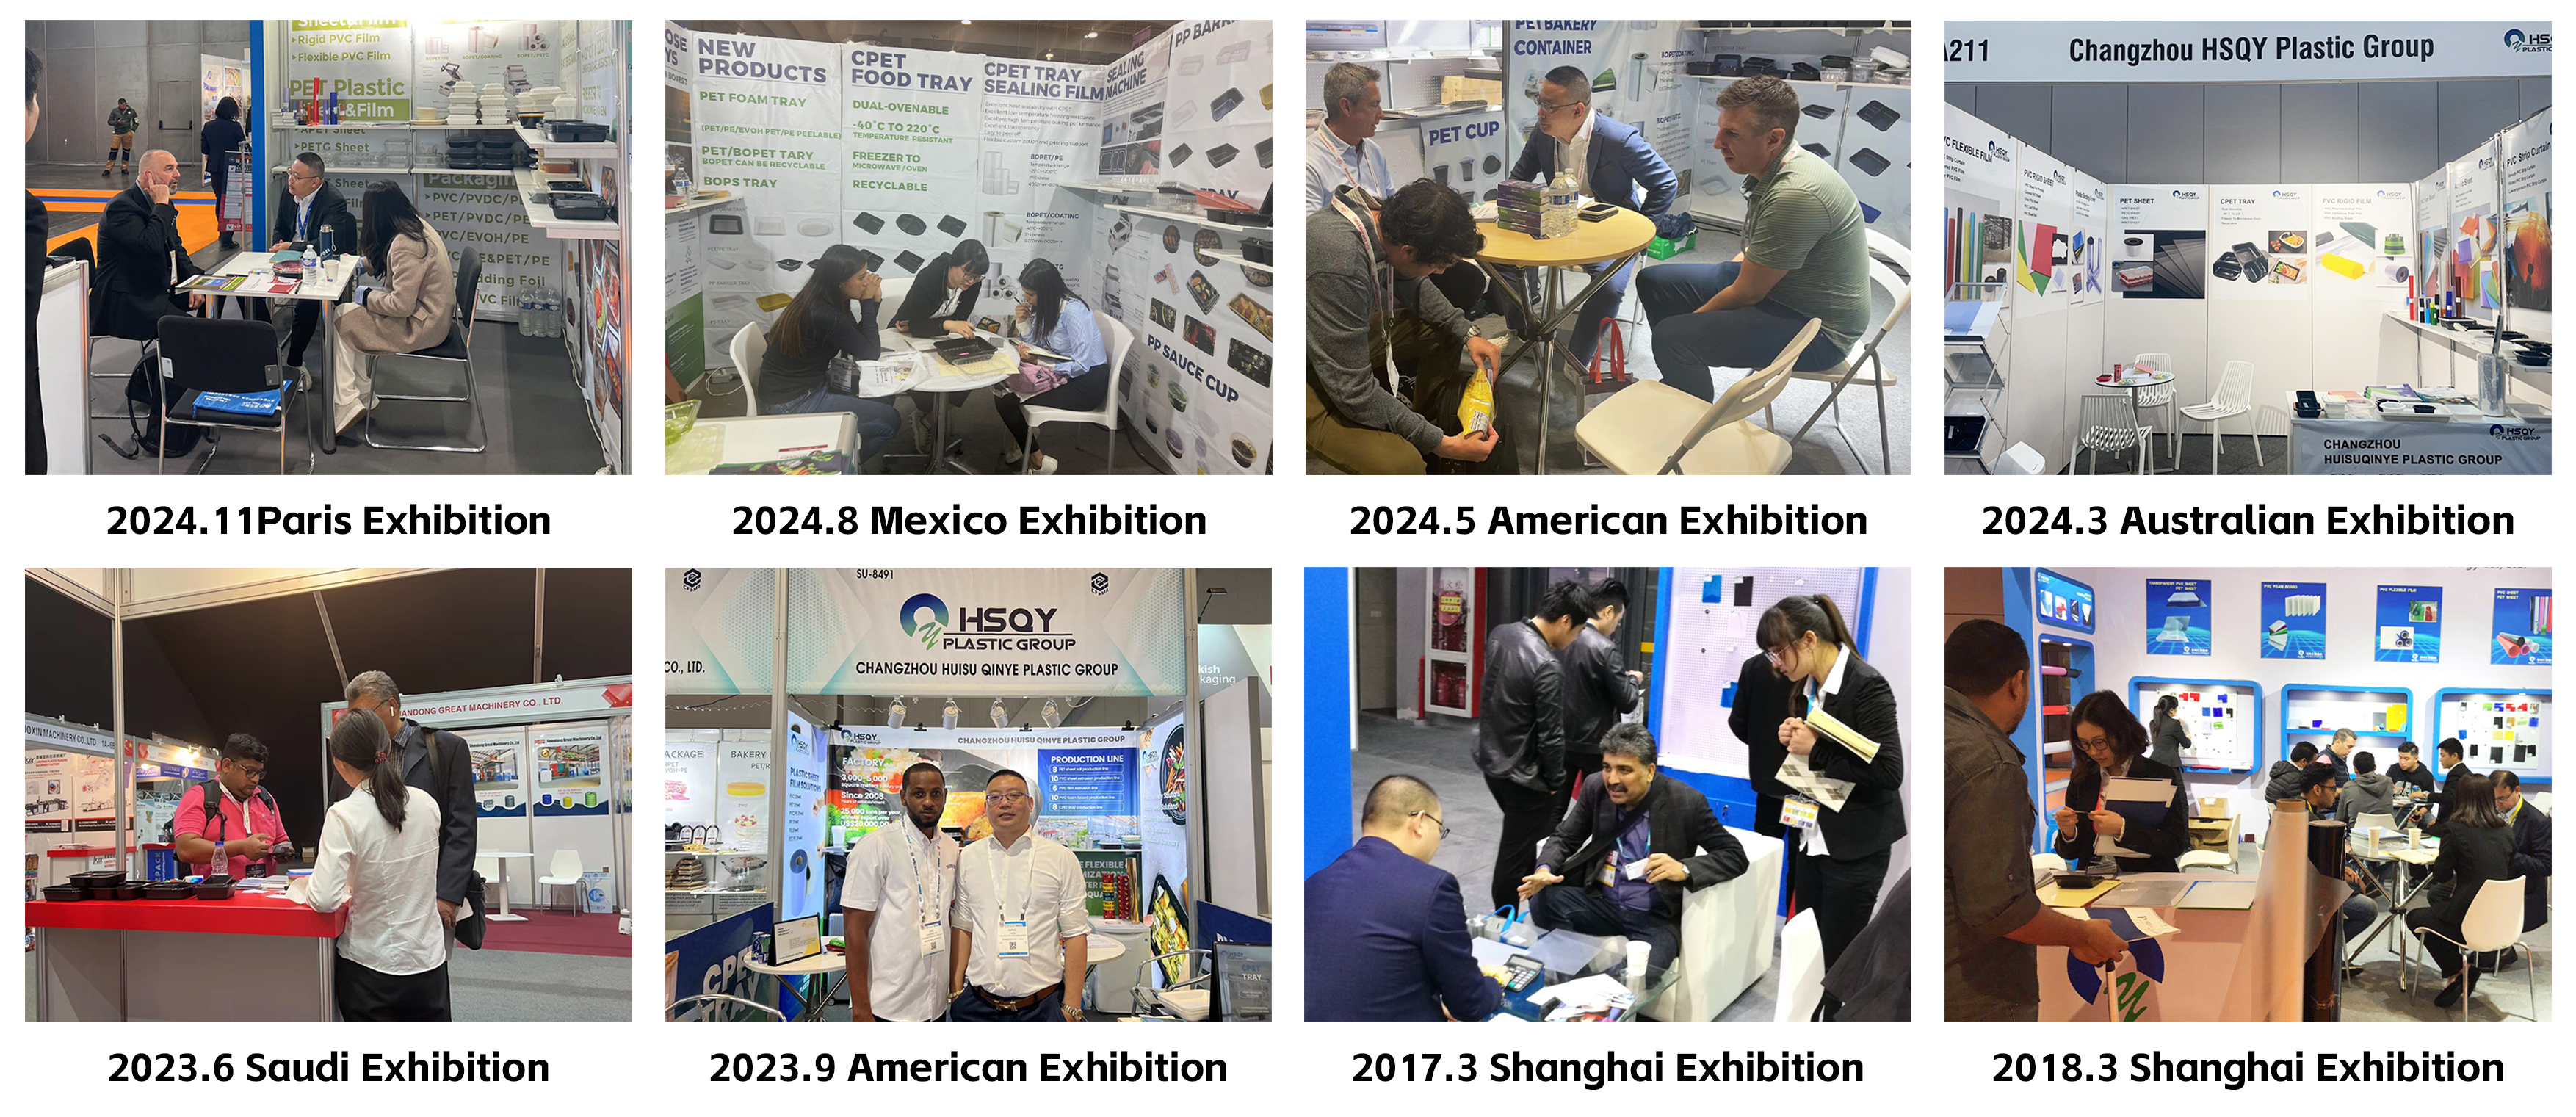
Global Exhibitions
HSQY Plastic Group participates in international plastics and packaging exhibitions and meets customers from thermoforming, packaging and industrial converting markets.

HSQY Plastic Group International Exhibition Activities
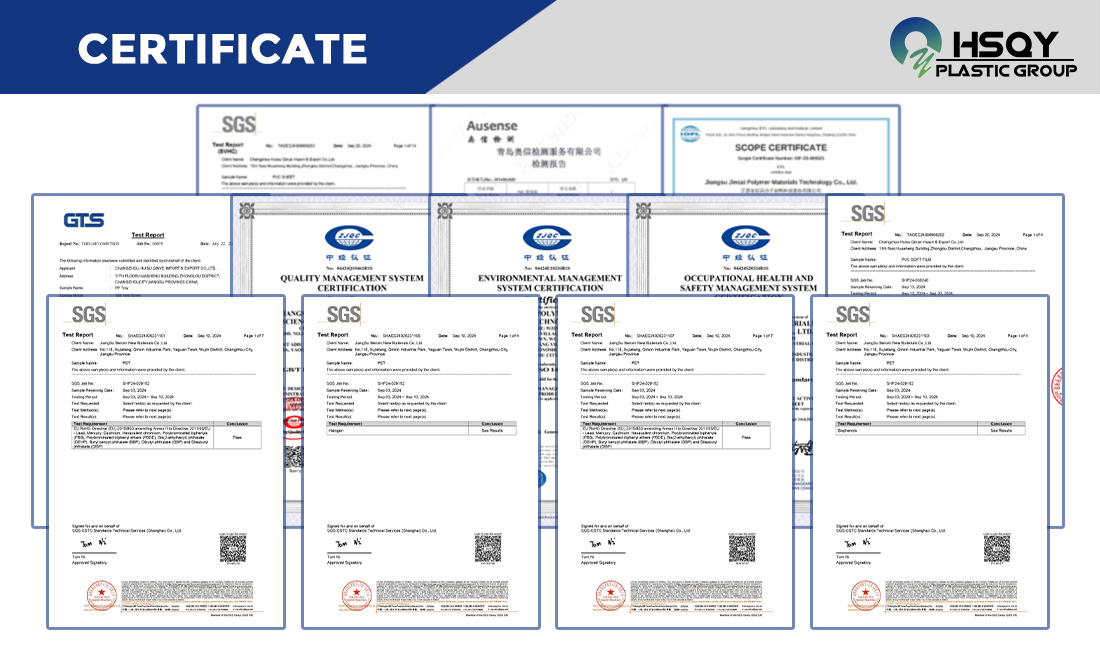
Certification & Documentation
The original product information references food, medical and electronics applications. The exact certification or compliance document required depends on the supplied PP grade and intended use.
Food-contact, medical, antistatic and other regulated applications should be evaluated using product-specific documentation rather than general company-level certification alone.
Why Source Vacuum Forming PP Sheet from HSQY?
HSQY supplies extruded polypropylene sheet in multiple thicknesses and customized widths for packaging and industrial converting applications.
For vacuum-forming programs, buyers can provide the machine specification, mold dimensions, starting sheet thickness, required width, optical requirements and end-use conditions so the material specification can be evaluated around the actual forming process.